
Turnkey Plant for Erythritol Production
From Concept to Commissioning – Your Trusted Partner for Erythritol Manufacturing
In today’s health-conscious world, the demand for natural, zero-calorie sweeteners is exploding. According to MarketsandMarkets, the global erythritol market is expected to grow from USD 250 million in 2023 to over USD 500 million by 2030, driven by the booming sugar reduction trend in food & beverage, nutraceuticals, and personal care.
But as the market grows, so do the expectations:
• Higher purity levels
• Lower energy consumption
• Greater process stability
• Faster return on investment
These demands are placing pressure on manufacturers—not just to produce erythritol, but to do it efficiently, sustainably, and at scale.
That’s where Myande comes in.
For over 23 years, we’ve been helping global manufacturers build and scale turnkey erythritol plants, combining cutting-edge fermentation technology, precision crystallization, and end-to-end process integration—all under one roof.


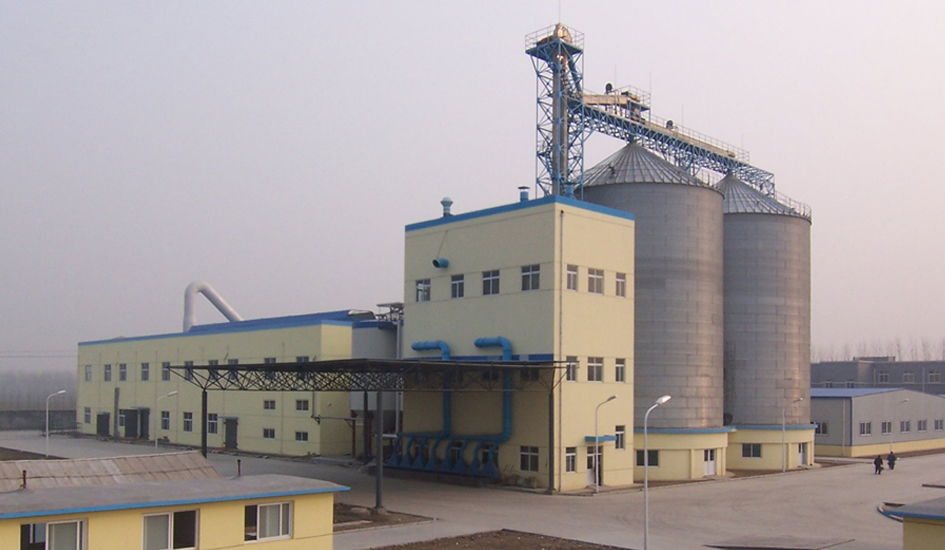
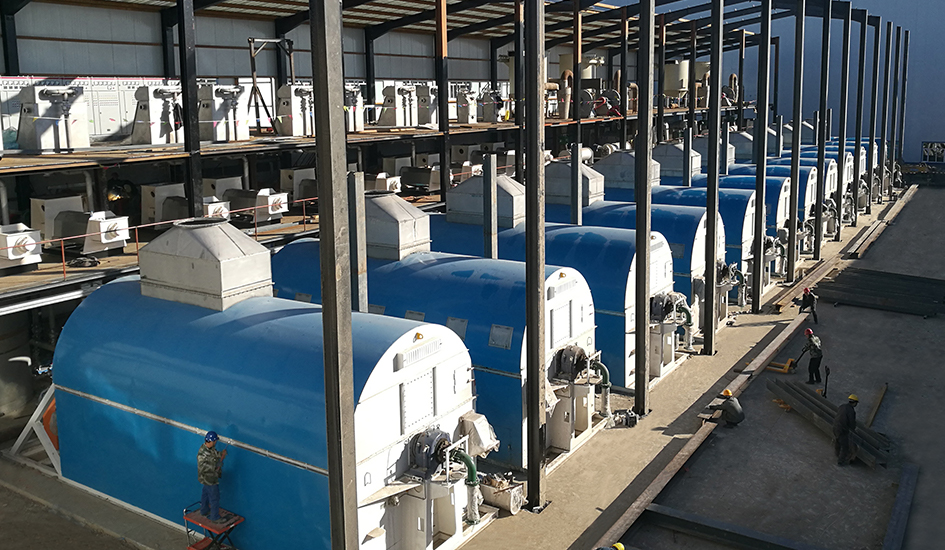
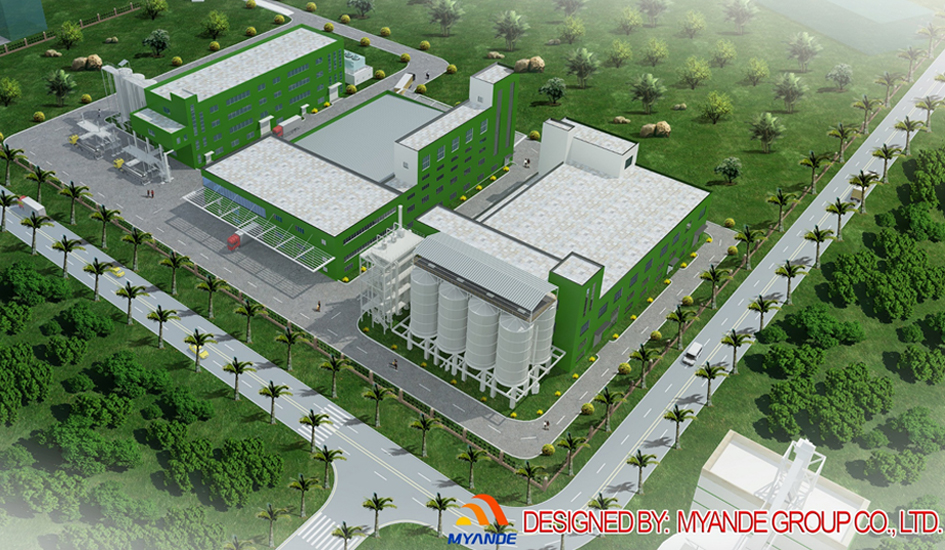
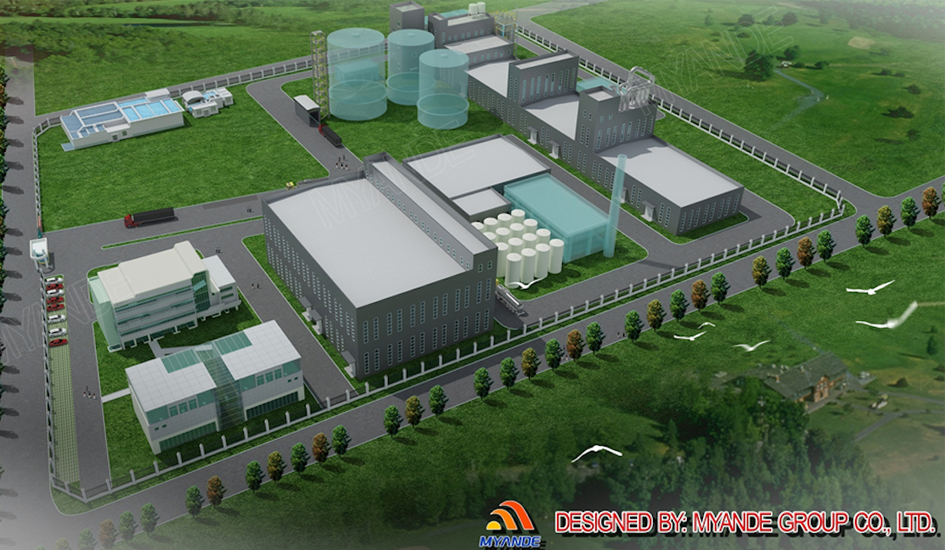
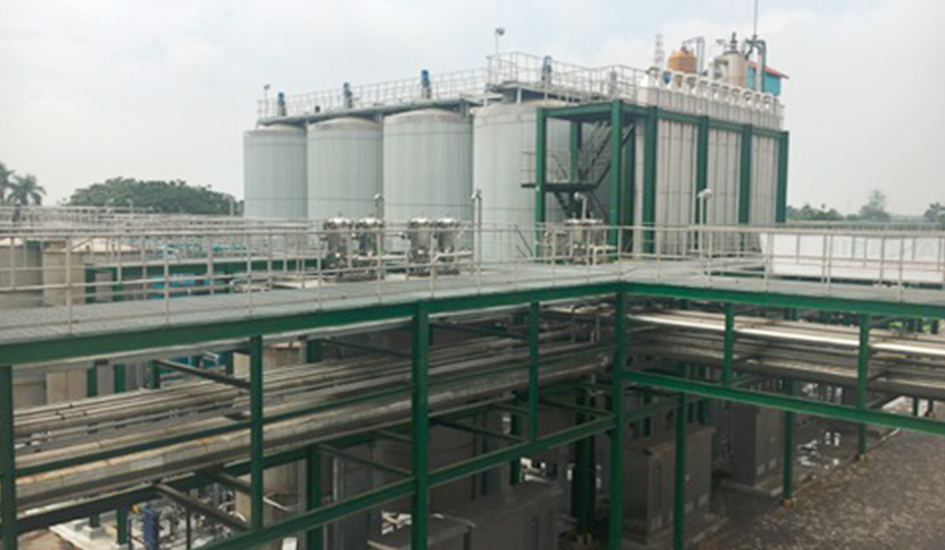

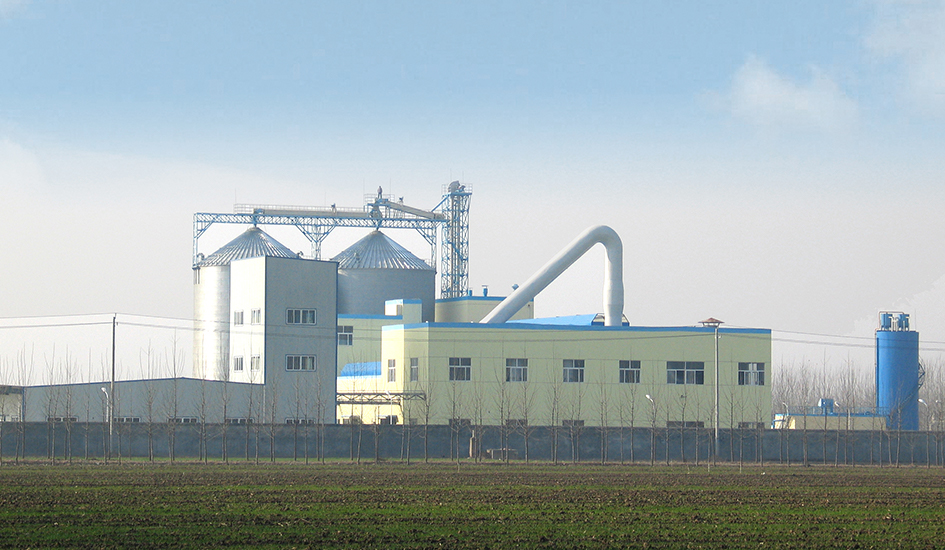
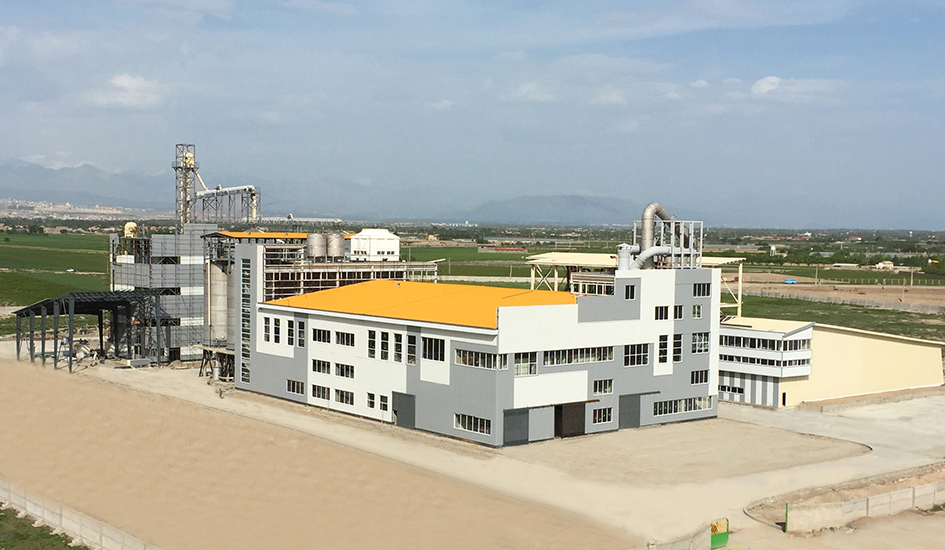
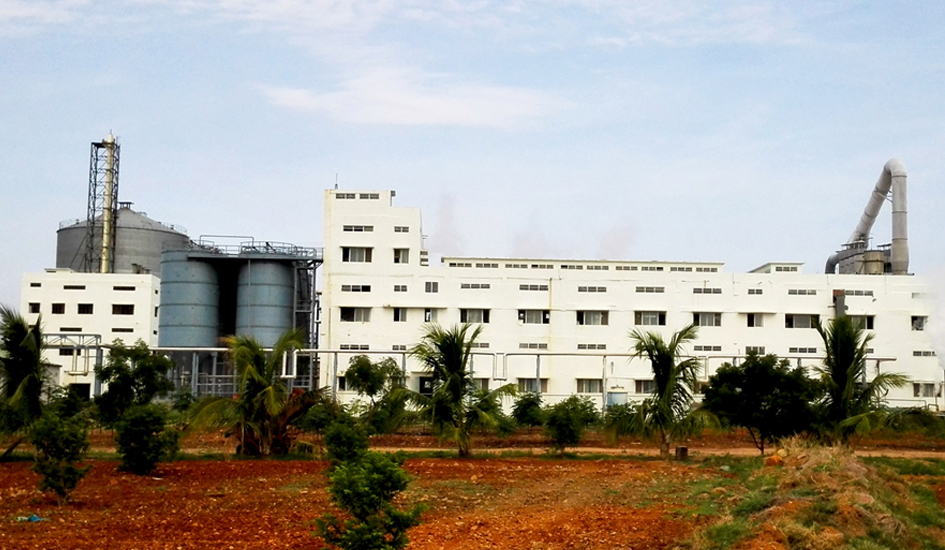
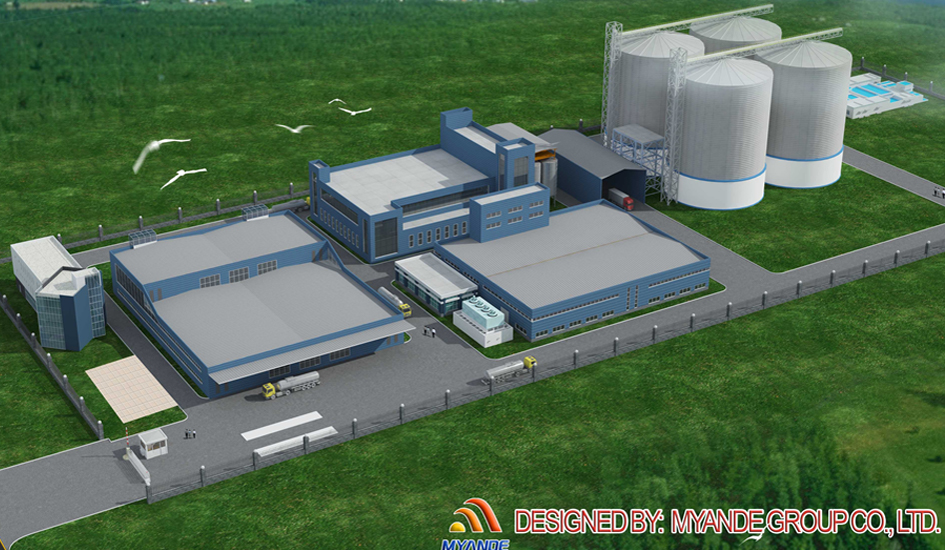
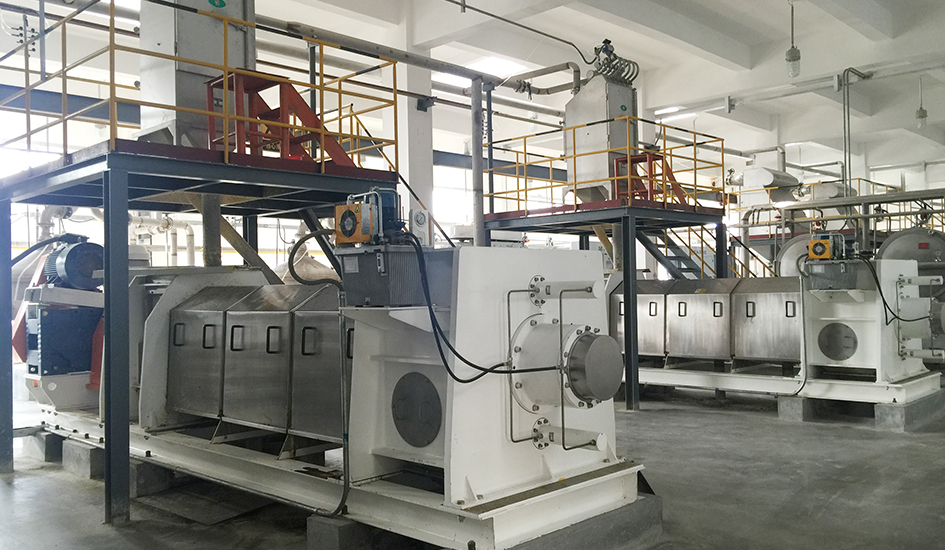

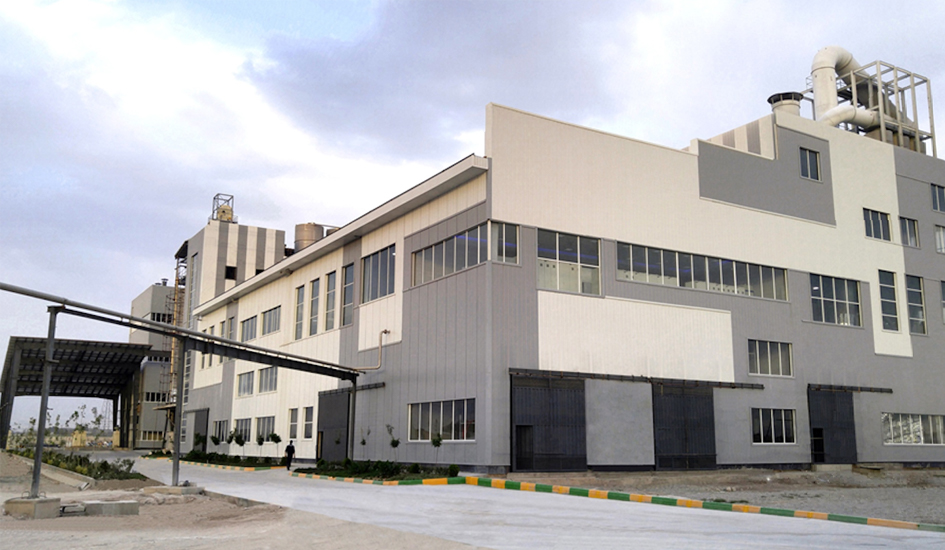
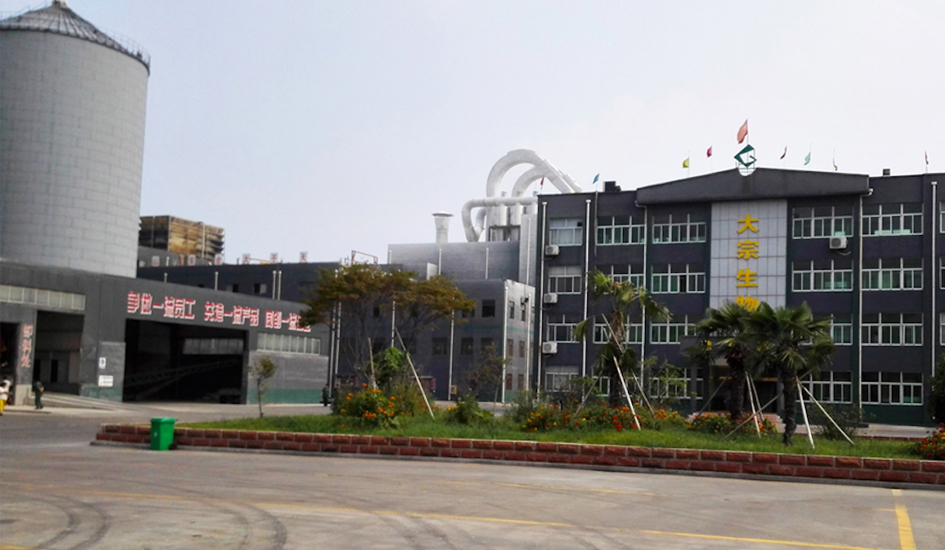
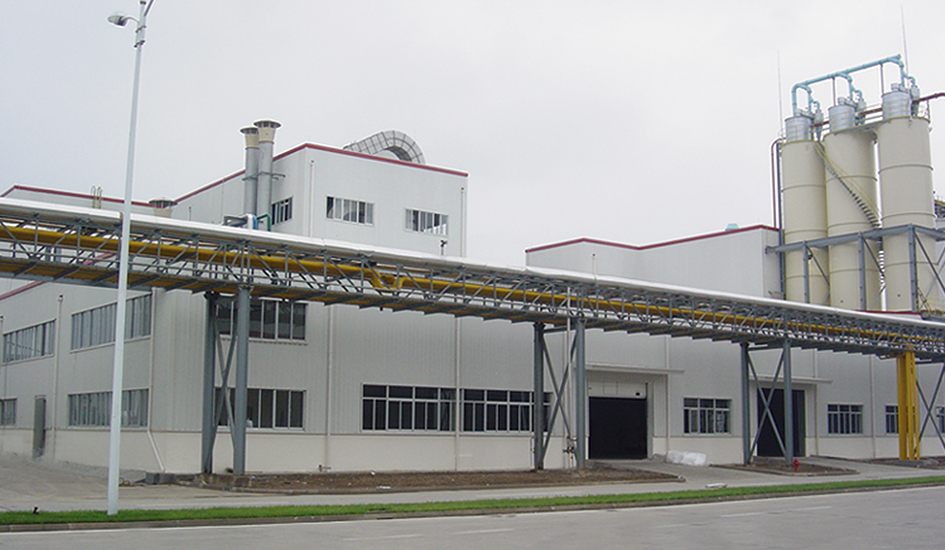
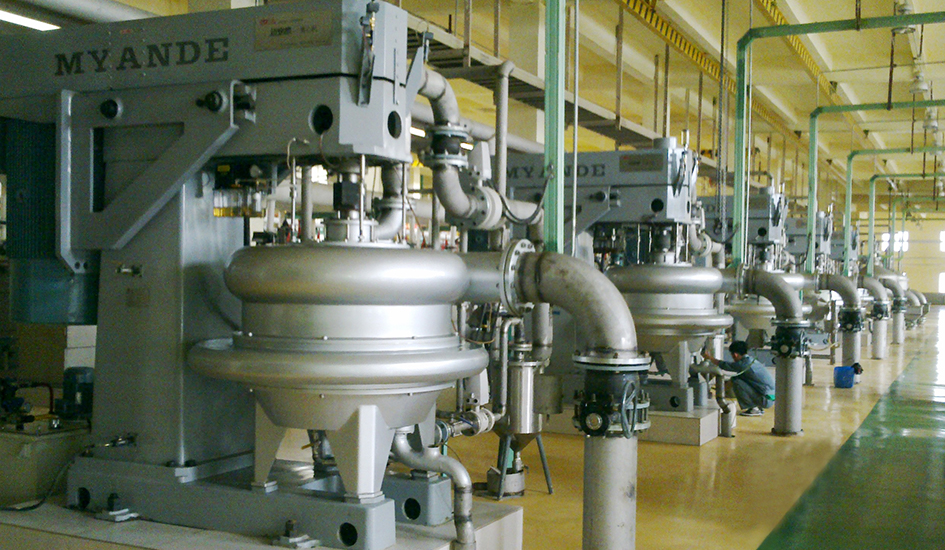
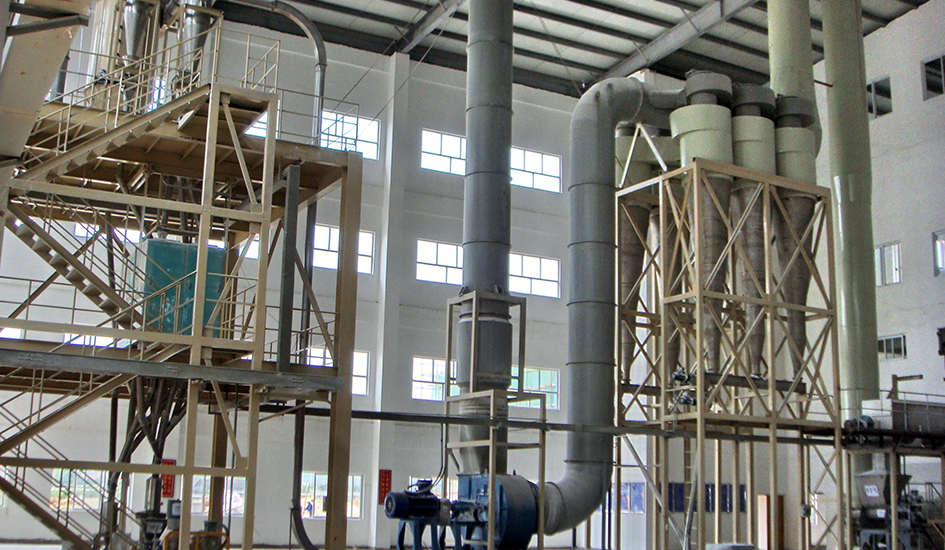
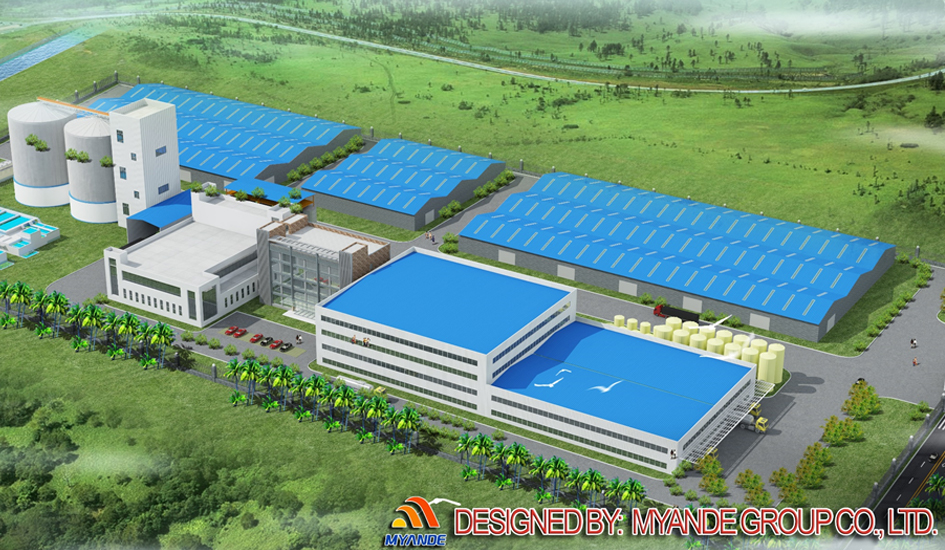

Your Erythritol Plant, Optimized from Start to Finish
We don’t just sell equipment—we deliver complete solutions that work in the real world.
Typical Erythritol Production Process We Design & Deliver:
1. Raw Material Preparation
Corn starch → Glucose syrup (enzymatic hydrolysis)
2. Fermentation
Using Moniliella sp. or Trichosporonoides sp. under controlled conditions
3. Filtration & Purification
Membrane separation, activated carbon treatment, ion exchange
4. Concentration
Multi-effect evaporation or MVR systems for energy-efficient concentration
5. Crystallization
Controlled cooling crystallization for uniform particle size and high yield
6. Separation & Drying
Centrifugation and drying (vacuum or spray) for final product
7. Automatic Packaging
Each module is custom-engineered for optimal performance, minimal energy use, and hygienic operation in line with FDA, CE, and GMP standards.

Why Global Clients Choose Myande for Erythritol Turnkey Plants
✔ Full Lifecycle Engineering Support
From feasibility study to factory commissioning—we're with you every step of the way.
✔ Deep Process Expertise in Fermentation & Sugar Alcohols
We specialize in bio-fermentation-based solutions. Whether you're producing erythritol, xylitol, or other polyols, we know what works.
✔ Proven Energy-Saving Technology
Our MVR evaporation, intelligent crystallization control, and CIP/SIP automation ensure lower OPEX.
✔ Custom Design, Not Copy-Paste
Each project is engineered to fit your raw material, target market, and local utilities.
✔ Local Training & After-Sales Service
Our job doesn't end with delivery. We offer hands-on training, troubleshooting, and remote diagnostics.

They trust and choose Myande
More than 1,600 complete plants have been supplied under Myande’s name in over 80 countries since 2003.
Behind every successful project is a great team. Our team is comprised of skilled individuals that share one common goal – Help our clients succeed.

What can we do for you?
We focus on supplying one-stop engineering service covering general layout plan, process design, R&D, equipment manufacturing, automatic control system, data integration, installation, supervision, commissioning, training and etc.
Our custom solutions come from a deep understanding of your needs, and we have the capability to complete each project from the design of the initial concept to manufacturing, installation, commissioning and delivery.
Solution Tailored to Your Needs

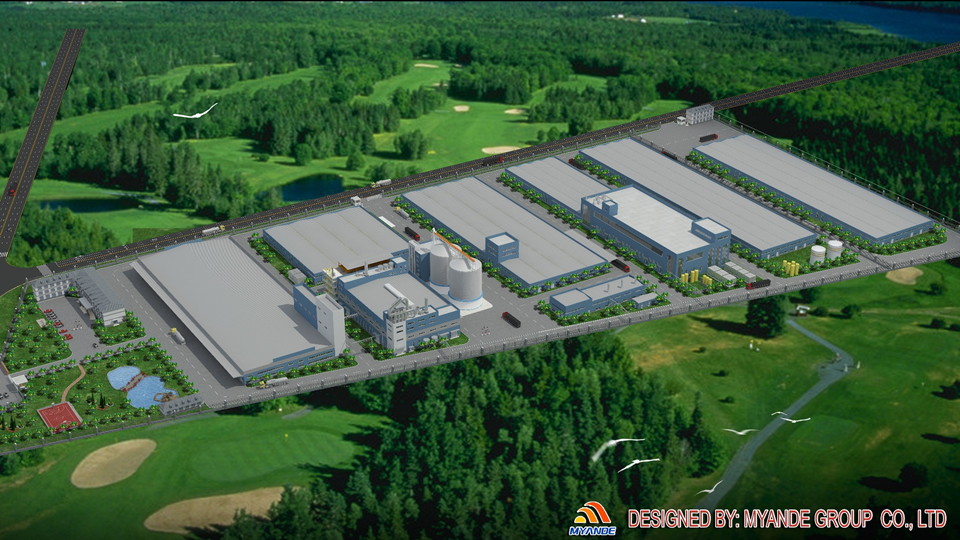
General Layout Plan
With a land prepared, the next thing you should consider is planning the general layout, which is a crucial foundation of a sustainable and cost-effective manufacturing.
Turn to us for help and we will present you the design for your plant by considering water, steam, electricity supply and etc.

Process Design
Combining our engineering expertise, industry know-how and practical skills with your knowledge, we provide the optimized and customized process design for your plant.

3D Plant Design
On the basis of plant layout design, combined with real situation, we can design a three-dimensional model of the entire plant. All the equipment, piping and instruments, any detail can be shown in the model, not only allowing you to have an intuitive understanding of the plant, but also providing overall information support for plant construction, equipment installation and future expansion.

Automatic Control System
We offer economical and most effective process automation solutions for the entire production line. Our RES automatic control system is developed based on PLC/DCS system.

Data Integration
From the perspective of the overall operation of the factory, Myande intelligent data integration management system collects basic data from raw grain procurement, warehousing, processing, inventory, sales and logistics, relying on the interconnection network system of each workshop. It provides real-time, accurate and traceable data reports for the current storage, processing and shipping.

Equipment Manufacturing
We owns in-house manufacture base of more than 130,000㎡ integrating R&D, production, project management which represents advanced engineering capability in the industry.

Installation and Commissioning
After finishing the installation of all machines, we offer on-site commissioning service to ensure compatible functioning.
Every move of the machine needs strong technical support from our experienced engineers. The only principle is that you can start manufacturing right after the commissioning.

Training and After-sales Service
Myande 360° Service Portfolio covers all your needs throughout the life cycle of your project. By minimizing your total cost of ownership, we help you stay ahead of the competition.
About Myande
Myande Group is a globally leading supplier of complete plants, equipment, and services for Oils & Fats, Starch & Derivatives, Fermentation, Evaporation & Crystallization, Material Storage and Handling and Smart Factory industries.
Myande Group currently has 1,600+ employees including 800 technical staff and 800 manufacturing workers. More than 1,600 complete plants have been supplied under Myande’s name in over 80 countries since 2003.
World-leading manufacturing base
In-house manufacture base of more than 130,000㎡ that integrates R&D, production, and project management, representing world-class engineering capability in the industry.

No Compromise on Quality
We are highly committed to Quality Assurance.
Our facilities and processes adhere to the highest local and international industry standards and certifications and are audited regularly for compliance.
With a global quality management system, we ensure that our customers all over the world receive high-quality, reliable products and solutions. We are well aware that our equipment have to function safely and efficiently for decades.
To effectively carry on the spirit of artisanship, improve the overall quality of front-line employees, we hold the “Workmanship Skills Competition" every year.


Certificates & Patents
At Myande, innovation is the result of the total process of developing an idea into a product or a new way of working which adds value to the business.
Over 600 registered patents and utility models demonstrate the company's innovation potential.

Our Global Presence
We focus on supplying one-stop engineering service covering general layout plan, process design, R&D, equipment manufacturing, automatic control system, data integration, installation, supervision, commissioning, training and etc.
Our custom solutions come from a deep understanding of your needs, and we have the capability to complete each project from the design of the initial concept to manufacturing, installation, commissioning and delivery.
You might also be interested in


Related Products


Lifecycle Service
Technical expertise and innovative products form the basis of your success. But we offer you even more: our extensive range of services gives you optimum support for your requirements and objectives in the long term.
Myande News & Insights

2,000TPD Rapeseed Crushing Plant Launched
Recently, a 2,000 t/d rapeseed crushing plant built by Myande Group for Daodaoquan Grain and Oil Co., Ltd. started operation successfully and started to yield qualified rapeseed oil and meal. Daodaoquan Grain and Oil Co., Ltd. is a comprehensive oil processing enterprise integrating production, scientific research, trade, warehousing and logistics of edible vegetable oil and its related by-products. This new rapeseed crushing plant incorporates a wide range of Myande core equipment possessing independent intellectual property rights, including the E-type extractor, hydraulic flaker, DTDC, conditioner, and other key equipment. To achieve flexible material incoming and discharging, Myande CCJL series sweep auger and CQJL series reclaimer are used. In addition, advanced energy-saving technology, negative pressure draining technology and intelligent safety technology are used to ensure the stable operation of the entire production line and excellent product index. With the concept of "creating the best performance for our customers", Myande cooperates with DaoDaoQuan to build a modern, energy-efficient, and environmentally friendly factory.

600,000 T/A Wheat Starch Deep Processing Project Successfully Launched
Recently, the 1st phase of Henan Hanyong's 600,000 tons (annual output) wheat starch deep processing project, designed by and installed under the guidance of Myande, has been smoothly commissioned, and contract for the 2nd phase was signed with Myande, marking the further extension of the domestic wheat deep processing industry chain. Henan Hanyong Biotechnology Co., Ltd. is one of the leading enterprises in agricultural industrialization of Henan province. It mainly produces edible alcohol with strong competitiveness and a high reputation in the market. Starch deep processing is one of Myande’s important business segments. After years of technology and experience accumulation in the field of starch deep processing, Myande has formed a complete set of production design system with a high degree of automation, stable operation and high product quality. In recent years, Myande has successfully established long-term strategic cooperative relations with multiple famous domestic and international enterprises. Combining with Hanyong's own industrial advantages, after in-depth research, efficient communication and repeated demonstrations, Myande has designed a set of production plan (as shown in the following figure) specially for the customer, and it can not only produce gluten and wheat starch, but also make better use of the mixed nutrient solution of process water and pentosan to produce alcohol, which will bring considerable economic benefits. The 1st phase project is a 500tpd wheat flour processing project, including a 3tpd gluten drying system and a 12tpd starch drying system. From beginning to end, the whole project lasted for 10 months. During the whole implementation process, from the plant layout planning, process design, intelligent automation design in the early stage, project service in the mid-term, to the installation, commissioning and training in the post stage, Myande’s rigorous, attentive and efficient one-stop service has won the unanimous praise of Hanyong. Through the joint efforts of Myande and Hanyong employees, a brand-new starch deep processing production line was successfully commissioned and started running smoothly, and all indicators were superior to the technical level of the same industry. In view of the pleasant cooperation in the 1st phase, Hanyong decided to cooperate with Myande again to expand its wheat starch deep processing output, and signed the 2nd phase project with Myande resolutely, namely 5t/d gluten drying system and 20t/h starch drying system. After which, Hanyong will become a high-quality gluten high-value conversion base with "the largest scale, the best environment protection and the highest level of research and development" in the industry in Asia.

Myande Awards 2022 “Spring Sunshine” Scholarship
In order to motivate employees' children to study hard and to enhance employees’ sense of belonging and happiness, on August 19, Myande held 2022 Myande Spring Sunshine Education Scholarship ceremony. Mr. Wangmu, vice chairman and Mr. Mao Weijiang, director in charge of manufacturing, participated in this ceremony and on behalf of the company presented scholarship stipends to children of Myande employees who are enrolled by four-year universities this year. In his speech, Mr. Wang highlighted that Spring Sunshine Scholarship is one of several company welfare benefits. It represents the company’s vision of moving forward with its employees and creating a better future together, and it reflects the company's care for the education of its employees' children and its high sense of social responsibility.
FAQ
-
What should I evaluate before investing in an erythritol production plant?
-
Start with the complete production economics rather than nominal plant capacity.
Key factors include glucose consumption, fermentation yield and productivity, fermentation cycle, downstream recovery, crystallization yield, steam and electricity consumption, water usage, and final product specifications.
For food-ingredient applications, crystal size distribution, purity, color, moisture, and batch-to-batch consistency should also be defined before process engineering begins.
The most useful investment KPI is ultimately the cost per ton of qualified, saleable erythritol, not simply fermentation capacity.
-
-
What are the biggest cost drivers in industrial erythritol production?
-
Glucose is a major raw-material input, but fermentation efficiency alone does not determine manufacturing cost.
Important cost drivers include:
- glucose consumption
- fermentation productivity and cycle time
- aeration and electricity demand
- downstream product recovery
- purification chemicals and water
- evaporation energy
- crystallization recovery
- mother-liquor losses
A competitive plant therefore needs to optimize both upstream fermentation and downstream recovery.
-
-
Why is oxygen transfer important in large-scale erythritol fermentation?
-
Industrial erythritol fermentation is an aerobic biological process, making oxygen transfer a critical scale-up parameter.
As fermenter size increases, mixing, dissolved oxygen, aeration, heat removal, and power consumption become increasingly interconnected.
Insufficient oxygen transfer can affect productivity and fermentation consistency, while excessive aeration or agitation increases electricity consumption.
A commercial plant therefore needs to optimize oxygen-transfer performance and energy consumption together, rather than simply increasing agitator power or airflow.
-
-
Why is glucose quality important for erythritol fermentation and downstream purification?
-
Glucose quality can affect both fermentation performance and downstream processing.
Impurities entering with the glucose stream may increase fermentation variability, purification load, color removal requirements, ion-exchange demand, and eventually product losses.
When starch is used as the original feedstock, the starch-to-glucose and glucose-to-erythritol sections should therefore be considered as one integrated production chain.
The lowest-cost glucose is not necessarily the lowest-cost feedstock if it creates additional downstream processing costs.
-
-
Why is downstream purification critical to high-purity erythritol production?
-
Fermentation broth contains microbial cells, residual substrates, salts, color-forming substances, other polyols, and metabolic by-products.
These impurities must be sufficiently removed before final crystallization.
Industrial purification may integrate solid-liquid or membrane separation, decolorization, ion exchange, and other purification steps depending on broth characteristics.
The objective is not maximum purification intensity, but achieving the required product quality with the highest practical recovery and lowest water, chemical, and energy consumption.
-
-
Why is crystallization one of the most important sections of an erythritol plant?
-
Crystallization determines not only product recovery but also crystal size distribution, downstream centrifugation performance, appearance, drying behavior, and final product consistency.
Poor supersaturation control may generate excessive fine crystals, while inappropriate cooling profiles can reduce crystal growth or increase product remaining in the mother liquor.
Myande integrates evaporation and controlled crystallization engineering to optimize concentration, supersaturation, cooling profile, residence time, and crystal growth, helping balance product quality with overall recovery.
-
-
How can mother-liquor losses be reduced without causing impurity accumulation?
-
Mother liquor may still contain economically valuable erythritol after primary crystallization.
However, simply recycling all mother liquor can accumulate other polyols, salts, color bodies, and fermentation-derived impurities, eventually affecting crystallization and final product quality.
The optimum strategy may involve controlled recycle, secondary recovery, additional purification, or selective discharge depending on the impurity balance.
The decision should be based on overall erythritol recovery versus additional purification, energy, and wastewater costs.
-
-
How can evaporation and heat integration reduce erythritol production costs?
-
Fermentation broth contains substantial water that must be removed before efficient crystallization.
Evaporation can therefore represent an important thermal load.
Depending on plant conditions, MVR, multiple-effect evaporation, condensate recovery, and process heat integration can reduce fresh steam consumption.
Myande integrates evaporation with upstream purification and downstream crystallization rather than designing it as an isolated unit, helping optimize both energy consumption and crystallization performance.
-
-
How can integrated process design reduce the cost per ton of erythritol?
-
Every section of an erythritol plant affects the next.
Low-quality glucose can increase fermentation and purification costs; poor fermentation selectivity increases downstream impurity load; excessive purification can reduce product recovery; and inefficient crystallization leaves valuable erythritol in the mother liquor.
Myande integrates glucose preparation, fermentation, separation, purification, evaporation, crystallization, drying, utilities, and automation as one complete production system.
The objective is to maximize qualified erythritol recovered from each ton of glucose while minimizing energy, water, chemicals, and product losses.
-
-
What should I compare when selecting an erythritol turnkey plant supplier?
-
Do not compare suppliers only by fermentation volume, nominal capacity, or initial CAPEX.
Request comparable indicators covering:
- glucose consumption per ton of erythritol
- fermentation yield, titer, and productivity
- fermentation cycle
- downstream recovery
- crystallization yield
- finished-product purity and crystal specifications
- mother-liquor management
- steam and electricity consumption
- water and chemical consumption
- wastewater generation
- automation
- pilot validation and industrial scale-up capability
The key question is: How much consistent, saleable erythritol can the complete plant recover from each ton of glucose, and at what lifecycle cost?
-
Contact Us
Contact us to see how we can help you grow your business.
Find the solution to an optimized future.
Contact Us
Product Information
Quantity
Unit
Piece
Support order samples, customization, wholesale direct, and complete payment. If the product you look for does not have corresponding customized content, pls fill out the form below to contact us, and we will reply ASAP.